Engineered for seamless off-site assembly, structural durability, and extreme climatic thermal performance. Manufactured under strict ISO quality standards.
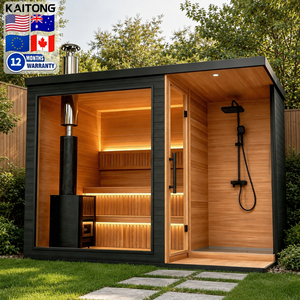
Premium Finnish pine & Red Cedar exterior modular sauna unit engineered for commercial resort deployment and executive site retreats.
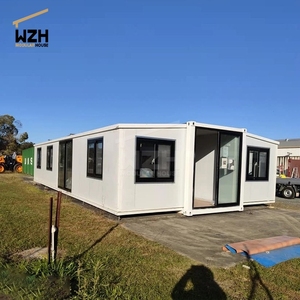
Heavy-duty expandable site headquarters featuring integrated kitchen, executive office spaces, and sanitary facilities.
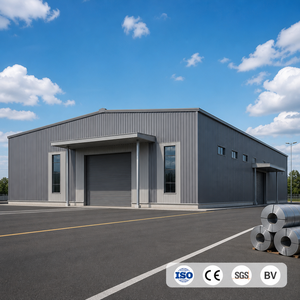
High-bay engineered steel framework designed for equipment logistics, heavy-machinery storage, and severe seismic zones.
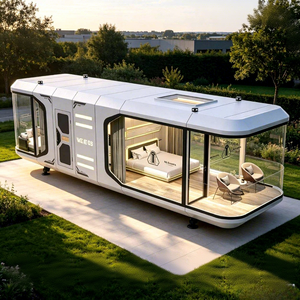
Futuristic aluminum-clad modular capsule pod optimized for high-end eco-resort hospitality and modern field offices.
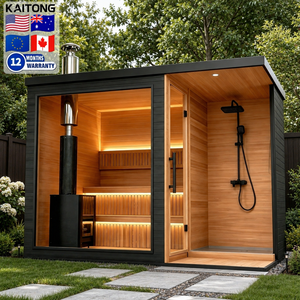
Heavy-duty timber cabin featuring traditional wood-stove heating and high-efficiency thermal insulation cores.
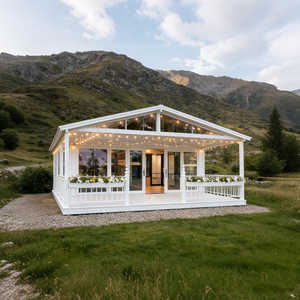
Rapid-deployment workforce accommodation pod with pre-fitted electrical wiring, thermal insulation, and multi-room options.
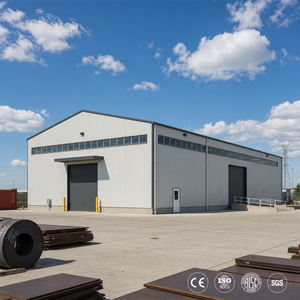
Custom structural steel manufacturing hall combining wide-span manufacturing areas with turnkey mezzanine office solutions.
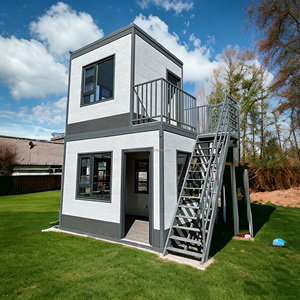
Standardized site office modular building featuring quick bolt-together framework, stackable up to 3 stories, high mobility.
An authoritative breakdown of material physics, structural integrity, thermal envelopes, and lean off-site modular construction methodology.
Modern mega-projects in infrastructure, mining, energy, and commercial real estate demand rapid, error-free site setup. As an established OEM manufacturing authority based out of our primary fabrication hub in IDA Jeedimetla, Hyderabad, TEXO Prefab World shifts over 80% of construction tasks from field operations into a controlled factory environment.
By leveraging automated CNC cutting, robotic welding, and rigid structural jig alignment, our modular site offices achieve fabrication tolerances tighter than <1 millimeter. This eliminates typical field misalignments, prevents water ingress along panel seams, and reduces on-site labor overhead by up to 65%.
Thermal control is paramount in severe environments—from scorching desert solar projects to freezing sub-arctic mining camps. Our OEM site offices are configured with high-density Polyurethane Foam (PUF) cores (40–42 kg/m³ density) or Polyisocyanurate (PIR) insulated sandwich wall panels.
This closed-cell insulation Matrix achieves thermal performance ratings exceeding R-25, lowering internal HVAC energy consumption by up to 30%. High-efficiency thermal breaks prevent condensation accumulation within internal wall cavities, safeguarding electrical distribution sub-systems from moisture damage.
Every commercial modular container cabin and custom site office is anchored on a cold-formed structural steel chassis composed of high-yield Q355B structural steel. Frame profiles undergo hot-dip galvanization with a minimum zinc coating weight of 275 g/m², providing exceptional resistance against atmospheric oxidation and industrial chemical exposure.
Engineered for high structural resilience, these frames accommodate dynamic floor loads exceeding 500 kg/m² and withstand lateral wind shear forces up to 150 km/h. The structural rigidity allows modular blocks to be safely stacked up to three levels (G+2) without requiring external structural skeleton reinforcement.
Heavy machinery and active construction noise require rigorous internal sound damping for administrative productivity. OEM wall configurations incorporate multi-layer rockwool acoustic cores achieving Sound Transmission Class (STC 45+ dB) isolation.
For life-safety compliance, structural core materials comply with Class A fire retardancy standards (EN 13501-1 / ASTM E84). Wall cores resist flame penetration for up to 60–120 minutes (EI60/EI120 ratings), allowing ample time for personnel evacuation during critical site emergencies.
Direct comparative parameters for site procurement engineers, project directors, and EPC procurement consultants.
| Structural Parameter | OEM Standard Specification | Custom Project Upgrade Options |
|---|---|---|
| Primary Steel Frame | Cold-formed Q235B Galvanized Steel Profiles (3.0mm - 4.0mm) | Heavy-Duty Q355B Steel Frame; Marine-Grade C5-I Anti-Corrosion Coating |
| Wall Insulation Core | 50mm / 75mm PUF Panel (40 kg/m³ density) | 100mm PIR Core / High-Density Rockwool Core (120 kg/m³, Class A Fire-rated) |
| Roof System Load | Integrated Drainage Gutters, Live Load capacity: 1.5 kN/m² | Reinforced Snow Load Package (up to 3.0 kN/m²); Solar PV Deck Mounts |
| Flooring Substrate | 18mm Fiber Cement Board + 2.0mm Commercial Homogeneous PVC Vinyl Sheet | Heavy-Duty Aluminum Checker Plate; Anti-Static Raised Access Flooring System |
| Fenestration & Doors | Double-Glazed Sliding PVC/Aluminum Windows (5+9A+5mm Tempered Glass) | Thermal-Break Aluminum Frames; Blast-Resistant / Bullet-Proof Glazing Units |
| Electrical Distribution | Pre-wired Hidden Conduits (CE/UL Standard), IP65 Distribution Box | Explosion-Proof Electrical Fittings; Smart Building Automation (BMS) Integration |
| Mobility & Lifting | Top Corner Castings (ISO 1161 Standard); Integrated Forklift Pockets | Quick-Disconnect Utility Couplers; Hydraulic Self-Unloading Legs |
Key industry shifts transforming off-site modular buildings from temporary accommodation into permanent, smart, net-zero corporate assets.
Global EPC contractors and Fortune 500 infrastructure firms are mandating strict Scope 1, 2, and 3 emission reductions across project lifecycles. Future OEM site office procurement strongly favors modular buildings utilizing low-embodied-carbon galvanized steel, recyclable aluminum envelopes, and zero-ODP (Ozone Depletion Potential) insulation blowers.
Factory-integrated roof-top solar microgrids and battery energy storage systems (BESS) allow remote site offices to operate off-grid with zero diesel generator reliance, transforming site administration into carbon-neutral hubs.
Next-generation site office cabins are transitioning into intelligent command posts. Integrated IoT sensor arrays continuously track internal indoor air quality (IAQ), ambient humidity, structural load stresses, and occupancy-based HVAC adjustments.
Plug-and-play modular telecommunication suites feature pre-installed 5G low-latency relay systems, fiber-optic distribution hubs, and automated biometric access control gates directly integrated into the modular frame prior to factory dispatch.
Procurement models are shifting from single-project disposable field structures toward circular multi-project fleet assets. Enterprise clients demand containerized flat-pack offices that can undergo rapid dismantling, flat-pack transport (with up to 4 flat-pack units packed into one standard 40ft ISO shipping container), and instant re-erection across subsequent project sites over a 25-year service life.
The integration of Building Information Modeling (BIM) level 5D directly into OEM factory production lines streamlines customized layout approvals. Procurement cycles are slashed from months to days as parametric design models feed CNC machinery directly, guaranteeing zero discrepancies between architectural floor plans and completed physical modular modules.
Backed by over 900+ successfully delivered projects spanning 50+ cities, our advanced manufacturing infrastructure delivers reliability, speed, and tailored structural execution.
Operating from our primary manufacturing facility at Plot No. 22, Phase-1, IDA Jeedimetla, Shapur Nagar, Hyderabad, equipped with heavy-duty robotic welding systems and Automated Roll-Forming lines.
Clients can inspect live volumetric models, material samples, and interior fit-outs at our flagship Experience Centre located near ORR Exit No. 03, Muthangi, Patancheruvu, Hyderabad.
Six dedicated product lines: Wooden Series (A-Frames, Arc Pods), Prefab Solutions (Villas, Site Offices), Portable Solutions (Porta Cabins, Bunkhouses), Specialized Structures (Clinics, Electrical Control Rooms), Security Guard Booths, and PUF Insulated Clean Rooms.
Because modules are 80%+ finished at the factory with complete interior electricals, plumbing, and surface finishes, final site erection requires only 7 to 10 days upon foundation completion.
Detailed answers regarding technical customization, shipping logistics, foundation requirements, and operational compliance.
We offer comprehensive OEM customization across dimension footprints (standard 20ft/40ft or custom non-standard lengths up to 12m), wall insulation thickness (50mm to 150mm PUF/PIR/Rockwool cores), internal partition layouts, integrated executive conference suites, double-glazed curtain walls, specialized anti-static flooring, and custom external branding color schemes matching corporate identity guidelines.
Prefabricated container offices and flat-pack units require minimal ground intervention compared to traditional masonry construction. A leveled concrete pad, strip footings, or elevated concrete pier blocks under the corner casting loading points are sufficient. This drastically reduces site civil costs and permits rapid installation on temporary leased land.
Units are optimized for global freight logistics. Flat-pack modular cabins are bundled into standardized ISO-dimension packages where 4 flat-pack modules match the external footprint of a standard 20ft ISO container. Alternatively, expandable cabins fold into self-contained steel shells safely transportable via standard flat-bed trailers or ocean freight dry vans.
With routine maintenance, our hot-dip galvanized steel framing and high-grade aluminum/zinc alloy coated steel wall panels deliver a design service life exceeding 25+ years. Structures feature replaceable modular wall panels, allowing easy repair or upgrades over extended operational lifecycles.
All structural framework designs undergo Finite Element Analysis (FEA) testing. Standard units are engineered to withstand wind loads of up to 150 km/h (Category 1 hurricane force) and seismic accelerations corresponding to Seismic Zone 4/5, making them significantly safer than traditional unreinforced brick masonry structures during natural disasters.
Partner directly with India’s leading modular building manufacturer. Connect with our technical engineering desk in Hyderabad to review custom floor plans, load specifications, and bulk volume pricing.